The most common mistake when choosing a hot stamping foil slitting machine is to focus on "maximum speed" and "price" when deciding. A device rated at 500 m/min, if the tension control system is not up to standard, may not even be able to maintain 200 m/min in actual operation; A machine priced over a hundred thousand yuan cheaper has a slitting accuracy difference of half a thread, and the foil wasted in a year is enough to make up the price difference.
The hot stamping foil is only 4~30μm thick, thin, brittle, and extremely sensitive to tension. Ordinary slitting machines can cause mild edges and misalignment, and at worst, the entire roll will be scrapped. The key to selection is to grasp three parameters that truly determine slitting quality: slitting accuracy, tension control, and tool system.
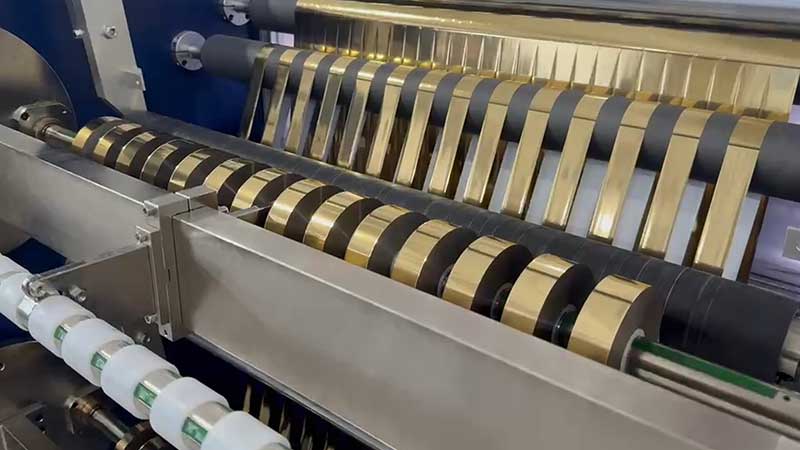
Parameter 1: Slitting accuracy—determines the lower limit of hot stamping registration
Slitting precision is a hard requirement and cannot be compromised. Ordinary hot stamping products allow an error of about 0.3mm, but in high-end packaging, cigarette packs, and luxury label fields, slitting accuracy must reach within ±0.1mm, and some high-end models can even reach ±0.05mm. If the precision is not met, misalignment and white exposure may occur during hot stamping, and the entire batch of products will be scrapped.
What guarantees accuracy? Two key points:
Whether the drive system is servo-based. Servo motor drives respond faster and more accurately than traditional variable frequency controls, and when combined with micron-level adjustable tool holders, each blade lands in its designated position.
Is the body rigid enough? High-rigidity cast iron or alloy steel bodies can effectively absorb vibrations during high-speed operation. Once the blade shaft radial runout exceeds 0.02mm, the cut will fluctuate in depth and shallow, forming wavy edges. When purchasing, you can request to use a dial indicator to measure the blade shaft runout—equipment with excessive bounce will inevitably have 'drift' accuracy at high speeds.
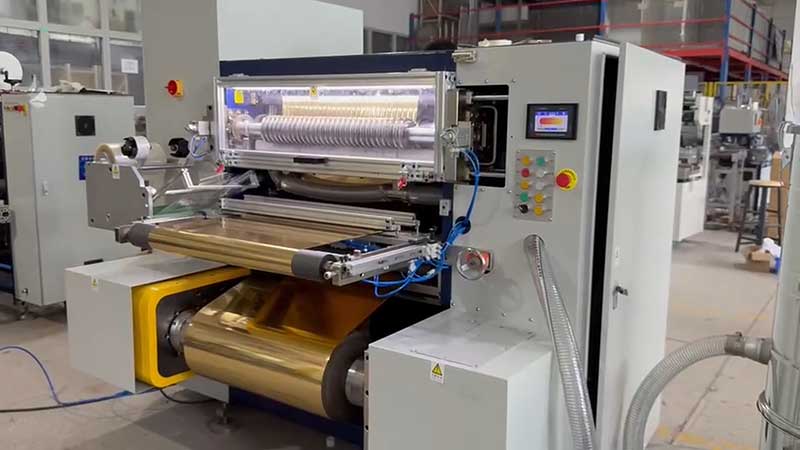
Parameter 2: Tension Control—The 'Lifeline' of Thin Material Slitting
The base material for hot stamping foil is PET film, with a thickness of 12μm thinner than a strand of hair. If the tension is slightly too high, the base film can be stretched and deformed, making it inaccurate to register during hot stamping; If the tension is slightly loose, it can curl up, wrinkle, or go off-balance. Over 90% of slitting size and end face misalignment issues stem from tension control.
To judge the quality of a tension system, look at three configurations:
Whether it is fully closed-loop servo control. The open-loop control reaction lags behind, causing large tension fluctuations during acceleration and deceleration. The fully closed-loop system uses sensors for real-time feedback and dynamic adjustment, controlling tension fluctuations within 3% of the set value.
Whether taper tension technology is available. As the winding diameter increases, the tension must decrease proportionally; otherwise, the outer layer may be extruded by the inner layer, causing the aluminum layer to transfer or stick. For hot stamping foils, taper tension is the core technology to prevent deformation of finished rolls.
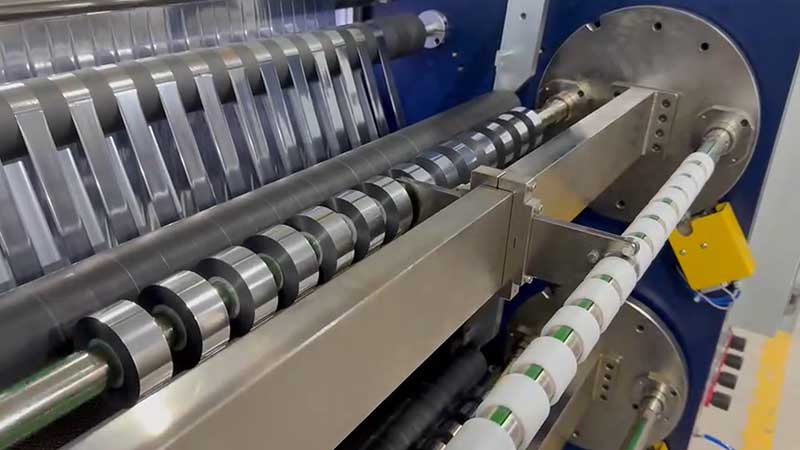
Whether the rewinding shaft uses a slip shaft or an air-expanding shaft. When winding multiple spindies simultaneously, slight differences in thickness of the cores can cause inconsistent tightness. The slip shaft allows each winding station to slide and adjust independently, solving the problem of inconsistent tightness between inside and outside.
If a device only mentions "maximum speed" but ignores tension control accuracy and taper curve, it can basically be concluded that it does not understand hot stamping foil.
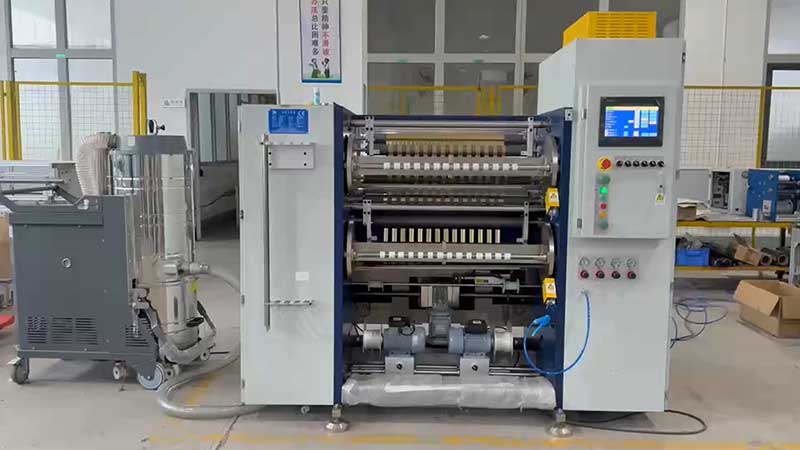
Parameter 3: Tool system—the ultimate executor of trimming quality
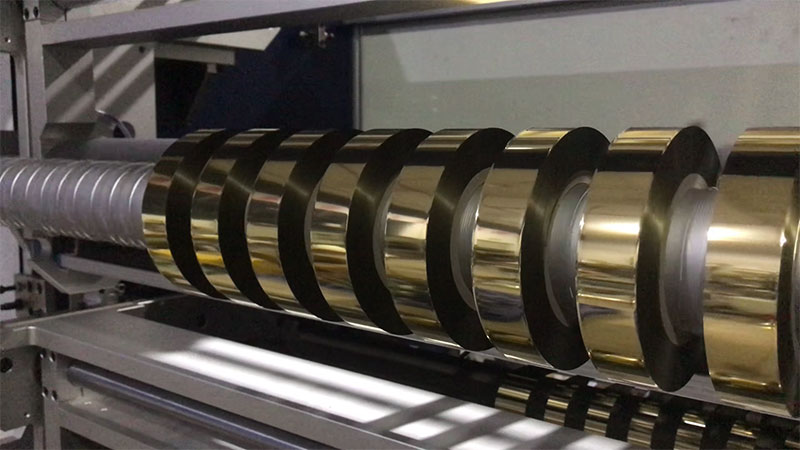
The hot stamping foil has a glue layer on its surface. Ordinary blades become glue and dull after prolonged use, and the edges cut are not "cut" but "squeezed" apart, inevitably producing burrs and foil powder. Burrs under hot stamping pressure directly appear as "gold edge defects," while aluminum powder falling onto the film surface forms "gold stamping spots."
How to choose a tool system:
Preferably slitting with a circular blade. The upper and lower disc blades are sheared, the cut surface is smooth and burr-free, the blades have a long lifespan, and are suitable for high-speed slitting (≥300m/min). Flat blades (razor blade type) are prone to wear that causes them to fail to cut or flange.
For tool materials, choose carbide or diamond coatings. These two materials have a long lifespan and are not prone to adhesive adhesion, so the edges require mirror polishing. The clearance and overlap between the upper and lower blades must be precisely adjustable—if the gap is too large, cutting will not be possible; if too small, it will accelerate wear.
Focus on dust removal and static elimination. The slitting process generates tiny aluminum powder and plastic dust, so a dust removal system combining contact (dust roller) and non-contact (ion air knife) must be equipped. Static elimination rods are installed at the coil release points to prevent static electricity from adsorbing dust into the coil.
Looking at all three parameters, they actually point to the same principle: the hot stamping foil slitting machine is not a general-purpose device, but a specialized machine. Using the standards of ordinary film slitting machines saves money on buying machines but loses money on material scrap and downtime.
Practical advice for selection: Bring your commonly used hot stamping foil master roll and test cut one roll on site. Check if the end face is as smooth as a mirror, use a high-power magnifying glass to check for microcracks on the cut edge, and observe whether the tension is stable during acceleration and deceleration. No matter how beautiful the specs are, why not actually cut it into a roll and see how it goes?
 English
 Deutsch
 Français
 Español
 Português
 日本語
 русский
 한국어
 عربي
 ภาษาไทย
 Tiếng Việt
 Italiano
 Automatic Foil Roll Cutting Machine
 1400mm Hot Stamping Foil Slitting Machine
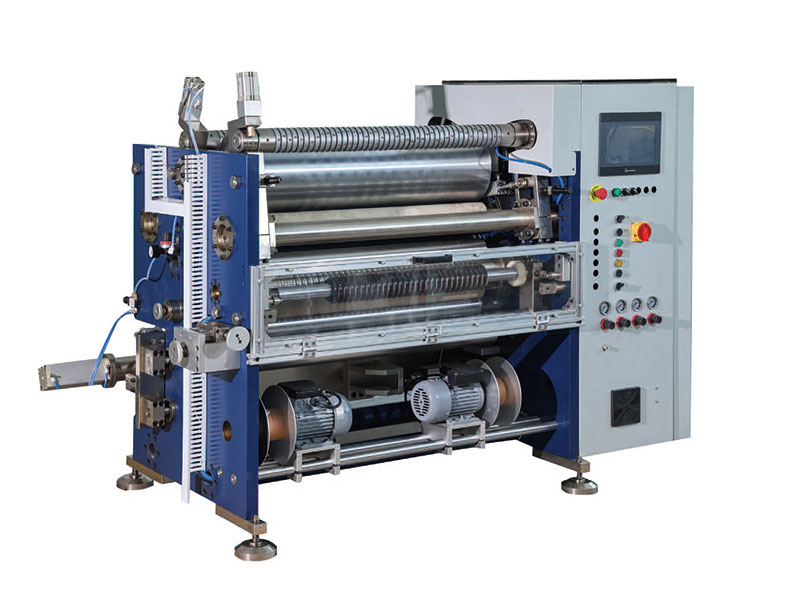 800mm Hot Stamping Foil Slitting Machine
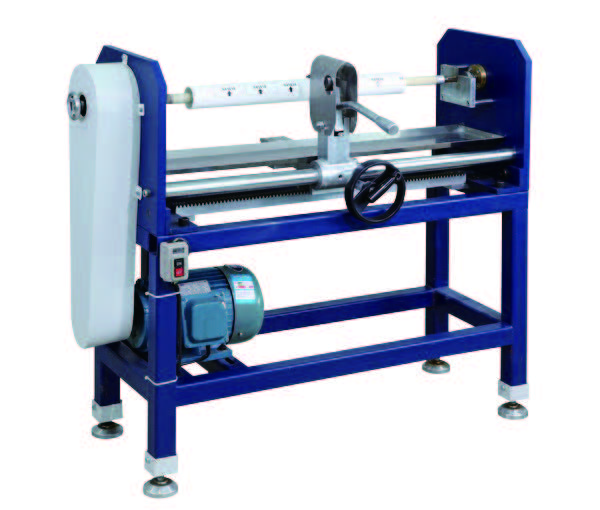 Manual Foil Roll Cutting Machine
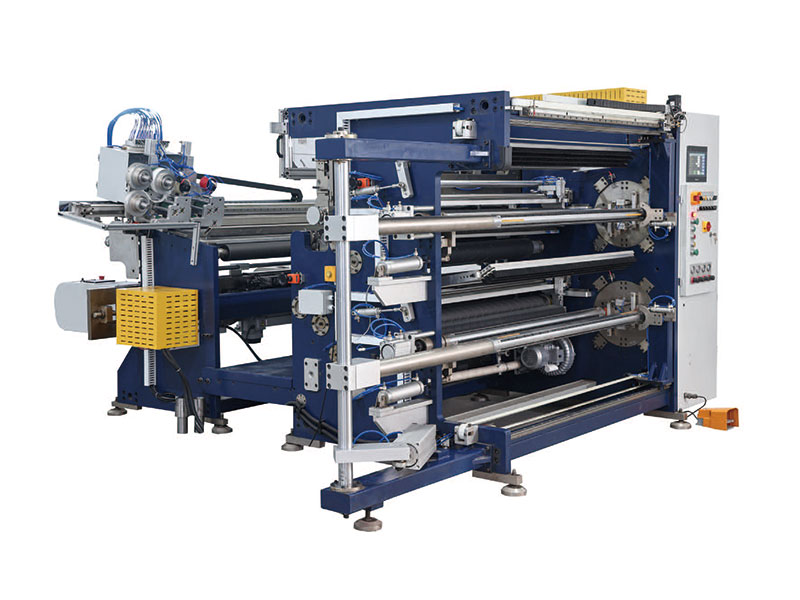 1350mm Hot Stamping Foil Slitting Machine
 Photo & Card Print Ribbon Rewinding Machine
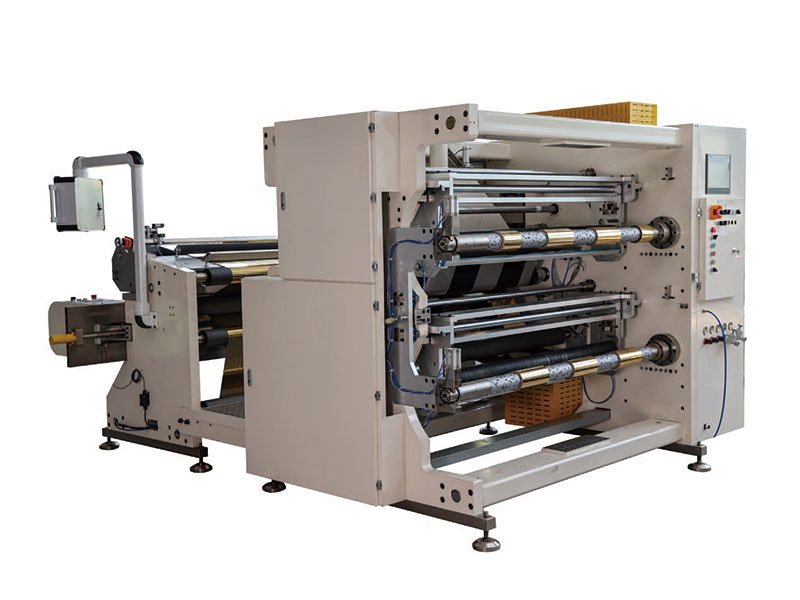 1400mm Copper Foil Slitting Machine
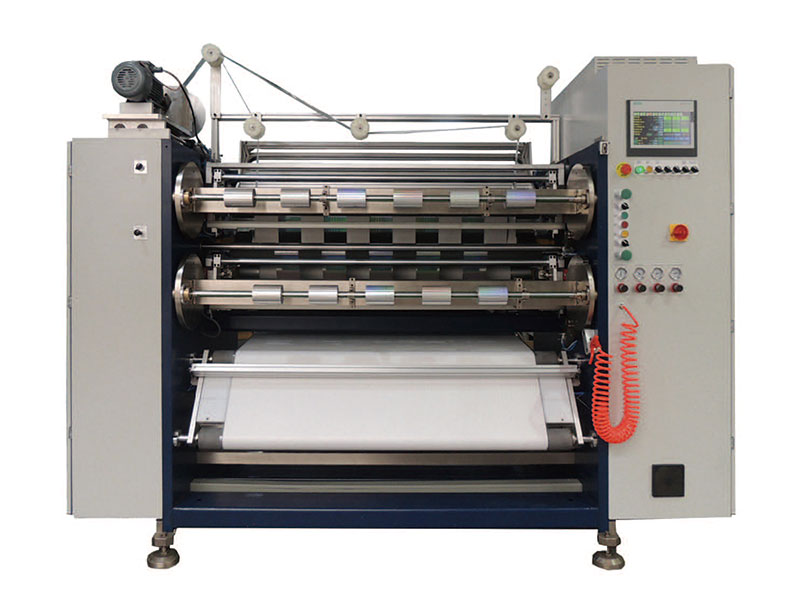 1350mm/1600 Foil Slitting Machine


 +86 135 9951 7291
 support@delishmachine.com
